Direct Factory OEM Manufacturing for Air-Cooled Condensing Units, Evaporators, and Insulated Panels.
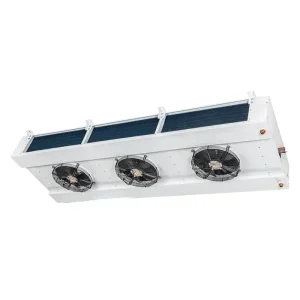
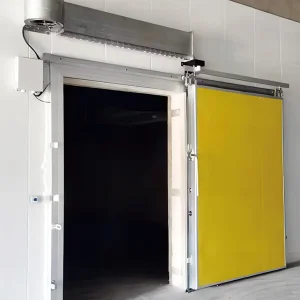
Comprehensive Thermodynamic Analysis, Fin-Tube Heat Exchanger Dynamics, and Custom OEM Manufacturing Architectures.
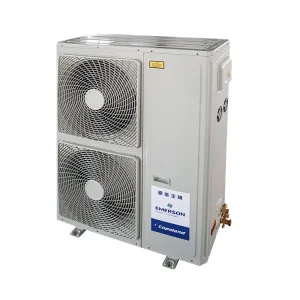
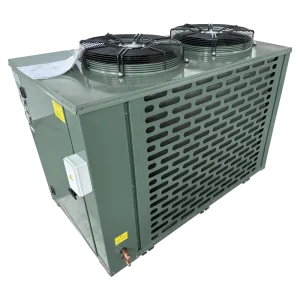
As a global leader among premier OEM Condensers Manufacturers, our engineering framework focuses on optimizing latent and sensible heat dissipation. Industrial condensers serve as the thermal rejection heart of vapor-compression refrigeration circuits.
By engineering advanced fluid dynamics within high-purity inner-grooved copper tubes and hydro-corrosion resistant aluminum fins, we achieve a Subcooling Margin Enhancement of up to 3.5K. This drastically decreases compressor energy consumption while mitigating flash gas formation before the expansion valve.
Transitioning from traditional round-tube plate-fin (RTPF) coils to state-of-the-art Microchannel Heat Exchangers represents a monumental leap in OEM condenser performance. Our factory utilizes multi-port extruded (MPE) flat aluminum tubes braze-jointed with corrugated zinc-coated aluminum fins.
This structural innovation yields a 40% reduction in refrigerant charge requirements and a 30% reduction in air-side pressure drop, allowing system designers to lower fan power demands while maximizing overall Coefficient of Performance (COP).
Operating in aggressive industrial environments—such as coastal logistics hubs, chemical processing plants, and marine freezing vessels—demands robust surface passivations. Our OEM condensers feature optional epoxy-coated, blue-fin hydrophilic, or cathodic electro-deposition (E-coating) treatments.
Tested under continuous ASTM B117 salt spray protocols exceeding 1,500 hours, our heat exchanger surfaces resist galvanic corrosion, maintaining structural heat-dissipation metrics over extended operational lifespans.
Inside Shaanxi YuanShengHeTong Refrigeration Equipment Co., Ltd. — Automated Production Lines and World-Class Quality Management.
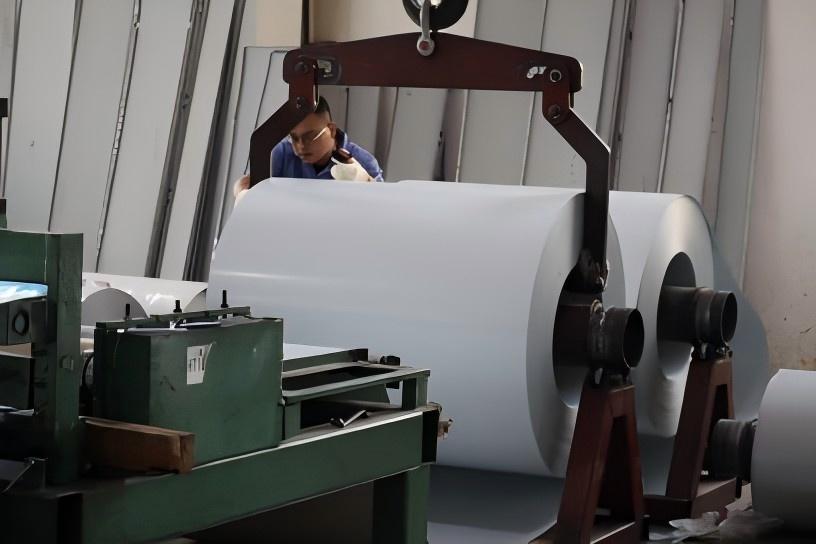
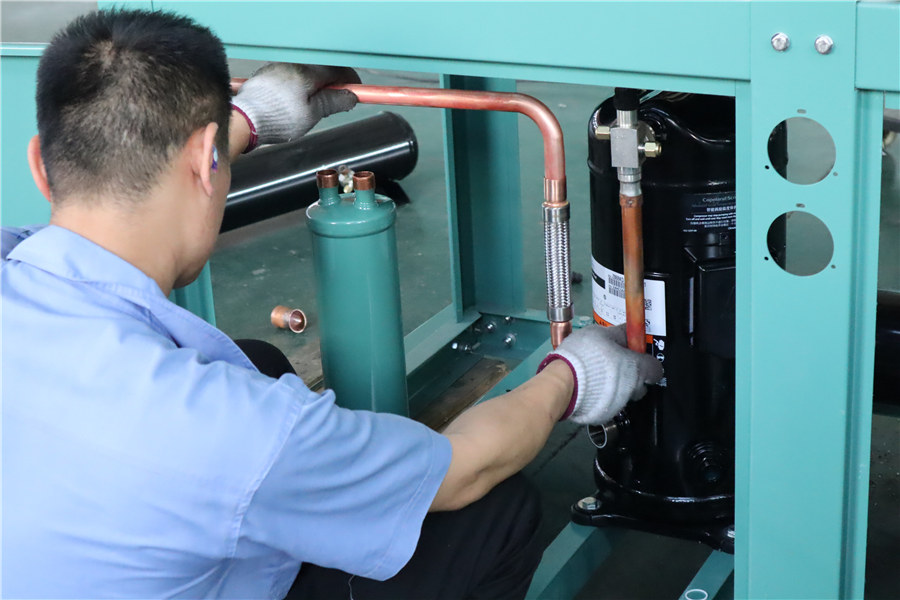
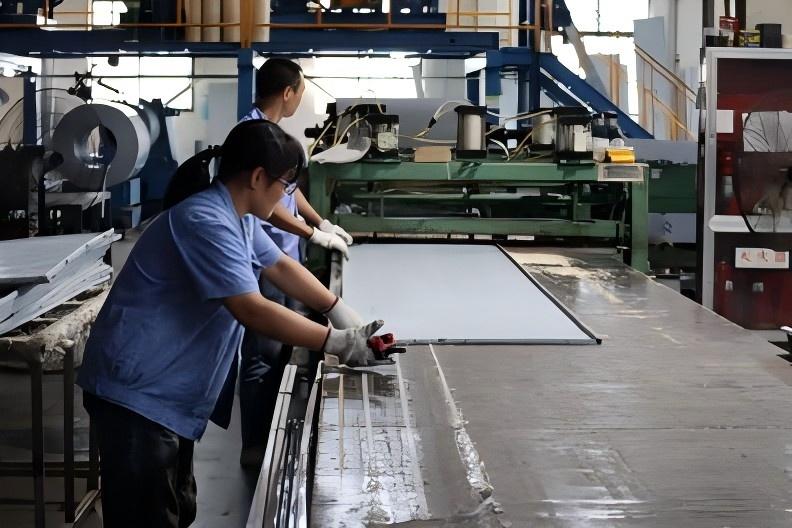
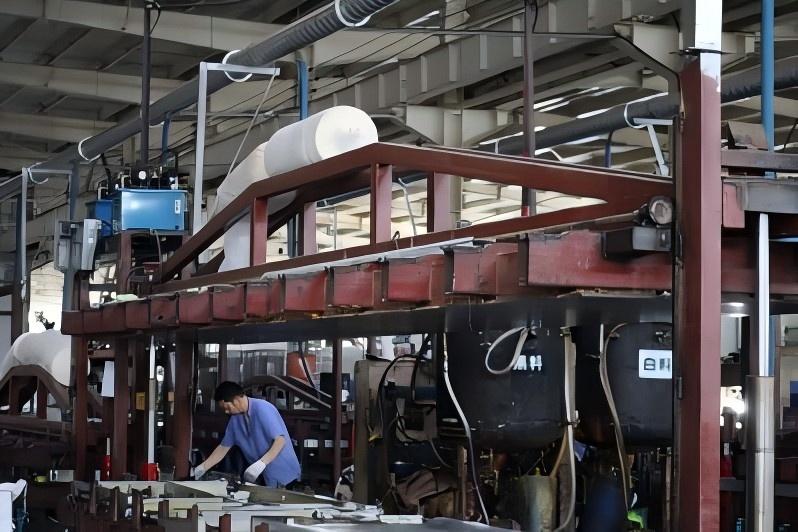
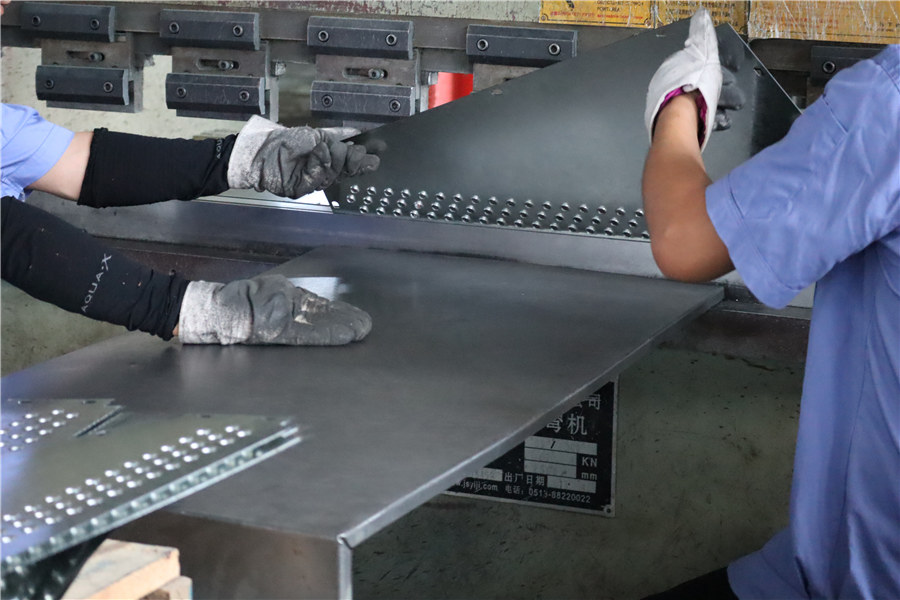
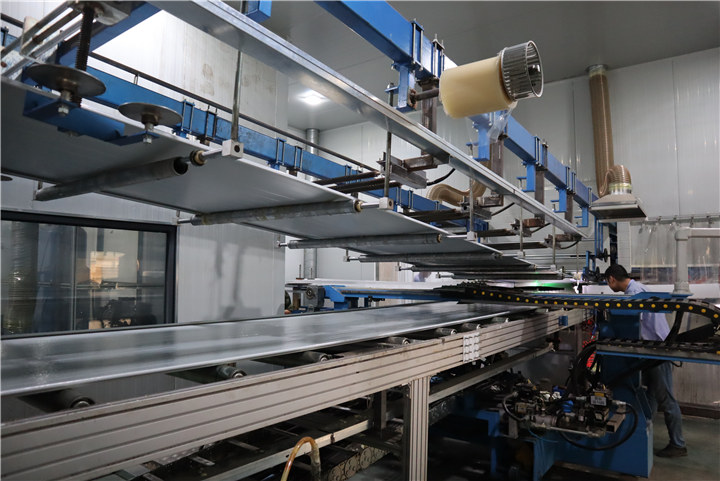
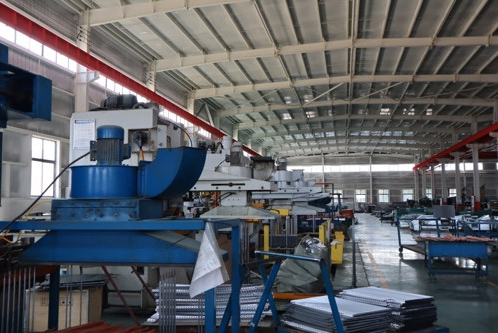
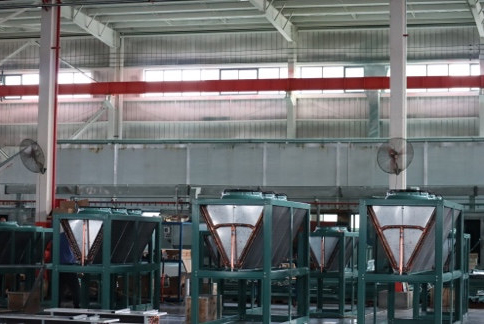
Our 60,000 square meter manufacturing campus incorporates 4 continuous standardized workshops equipped with high-speed automated fin punch presses, hairpin benders, CNC tube expansion machines, and automatic split-joint assembly systems.
By automating tube-to-fin mechanical expanding, we eliminate air gaps between copper tubes and aluminum fins, guaranteeing optimal thermal contact conductance. Our workforce of 180 certified technicians works alongside robotic welding stations to deliver zero-defect OEM condenser batches.
Quality control is non-negotiable. Overseen by an independent 10-person QC inspection team, every air-cooled condenser and condensing unit undergoes strict pressure testing using nitrogen immersion (up to 3.0 MPa) and helium mass spectrometer leak detection.
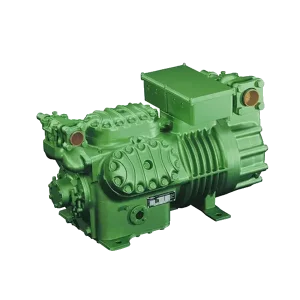
Through strategic raw material buffering (raw copper, aluminum coil stock, and branded scroll/screw compressors), we hedge against global commodity volatility, providing foreign OEM clients stable pricing and guaranteed delivery schedules.
Driving Energy Transition through Natural Refrigerants, Variable Speed Controls, and Smart AI Defrost Architecture.
Global environmental mandates (EU F-Gas III, US AIM Act) require rapid phase-down of High-GWP HFCs. Our R&D facility has re-engineered OEM condenser circuits to handle natural refrigerants such as Propane (R290) and Transcritical Carbon Dioxide (CO2 / R744).
Our ultra-high-pressure CO2 air-cooled gas coolers are rated up to 130 bar design pressure, equipped with specialized heavy-wall copper alloy (K65) or full stainless-steel headers to ensure absolute pressure boundary containment.
Future-proofing thermal infrastructure demands intelligent air management. We integrate Electronically Commutated (EC) fan motors featuring internal microprocessors with MODBUS/BACnet IoT connectivity.
EC fans adjust rotational velocity based on live condensing pressure feedback, reducing dynamic fan power consumption by up to 65% at partial load conditions while suppressing acoustic emissions in noise-sensitive urban installations.
For operations located in extreme ambient climates (Middle East, Southwestern USA, Southern Europe), standard air-cooled condensers suffer capacity degradation during peak summer conditions. Our hybrid adiabatic OEM condensers utilize high-efficiency evaporative pre-cooling pads.
During ambient spikes above 38°C, the system pre-cools incoming air via micro-misting, lowering dry-bulb temperatures closer to wet-bulb limits and preserving cooling capacity without scaling condenser fins.
Custom Engineering Tailored for Global Commercial, Industrial, Agricultural, and Pharmaceutical Cold Chains.
Biomedical logistics requires precise temperature maintenance (±0.5°C tolerance). Our custom OEM condensing units integrate redundant dual-circuit air-cooled condensers paired with scroll/screw compressors, emergency failover switches, and medical-grade PIR insulation sandwich panels.
Post-harvest agricultural cooling demands severe pull-down capacity to neutralize field heat in fruits and vegetables. We manufacture specialized high-air-throw condensers and electric/hot fluorine defrost evaporators engineered for high latent moisture management.
Multi-deck supermarket displays and central warehouse facilities require multi-stage rack condensing units. We manufacture floating condensing pressure control racks with VFD-driven fans to maximize year-round seasonal energy efficiency (SEER).
For marine vessels and coastal chemical plants, we build condensers featuring 316L stainless steel casings, copper-copper (Cu/Cu) coils, and heavy-duty IP66 waterproof fan motors capable of resisting salt mist and corrosive atmospheres.
Why Procurement Directors Choose Shaanxi YuanShengHeTong for Turnkey Thermal Systems.
We provide full structural customization (box-type, V-shape, W-shape, top-discharge, side-discharge) to match precise customer footprint requirements and mounting envelope parameters.
By engineering high heat transfer coefficients and low pressure drop circuits, our condensers lower ongoing kilowatt-hour consumption, providing payback on equipment cost within 14 operational months.
Every unit is assigned a digital serial code tracking factory raw material heats, automated soldering logs, nitrogen pressure hold graphs, and final QC sign-off certificates.
Meeting International Standards for Seamless Export & Site Integration.
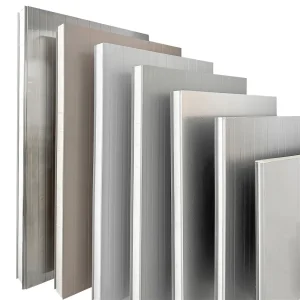
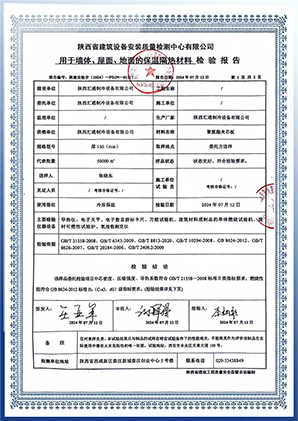
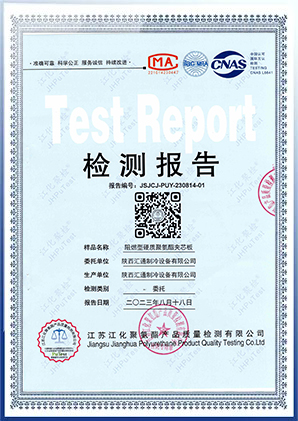
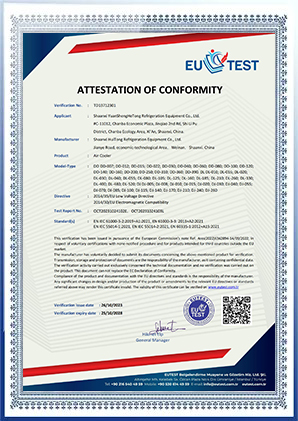
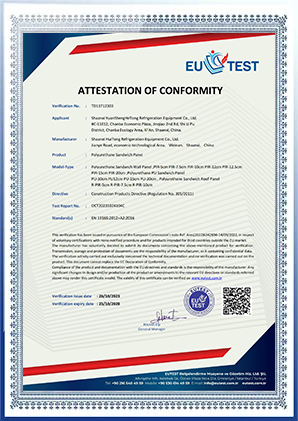
Our products comply with international regulatory frameworks including CE Mark, ISO9001:2015, ISO14001, and Pressure Equipment Directive (PED 2014/68/EU). All polyurethane and polyisocyanurate (PIR/PU) sandwich panels achieve B1/B2 fire retardancy ratings according to EN 13501-1 and GB8624 standards.
Equipment is pre-charged with protective dry nitrogen, sealed, and packaged in reinforced export-grade plywood crates or heavy-duty steel-skid frames. We supply full technical documentation, CAD dimensional drawings, circuit wiring schematics, and 24/7 remote engineering commissioning support.
A Premier Manufacturing Enterprise Specializing in Insulation Panels & Turnkey Refrigeration Machinery.
Shaanxi YuanShengHeTong Refrigeration Co., Ltd. is a professional factory and enterprise focusing on insulation panels and refrigeration equipment. Besides product manufacture, we also provide services like project design, construction, installation, as well as after-sales service.
We integrate "high quality products, one-stop project solution, engineering advanced services, and international trade" to provide customers with excellent products and satisfied services. Our involved professional fields include refrigeration of fruits, vegetables, food industry; also refrigeration of large supermarkets, restaurants, hotels, medical and logistics companies etc.
Our business in refrigeration fields started in 1996, with more than 20 years experience in refrigeration industry, we are confident in our professionality. And our factory is specializing in refrigeration manufacturing and technology.
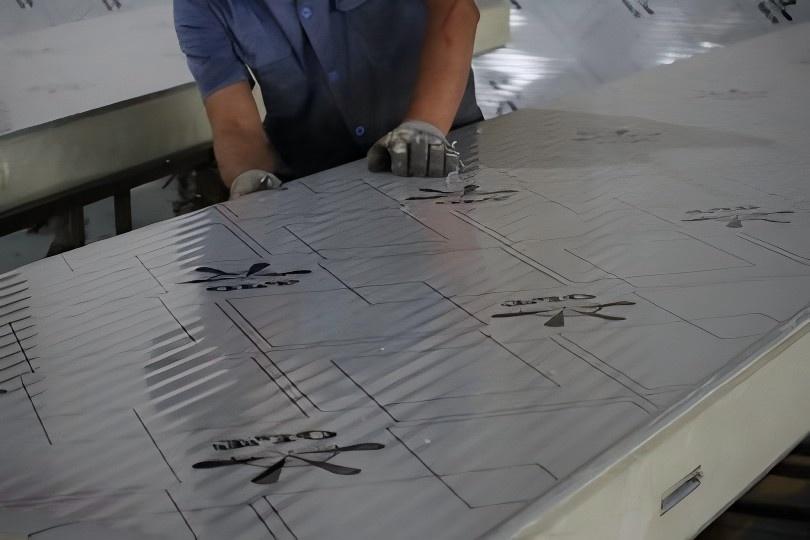
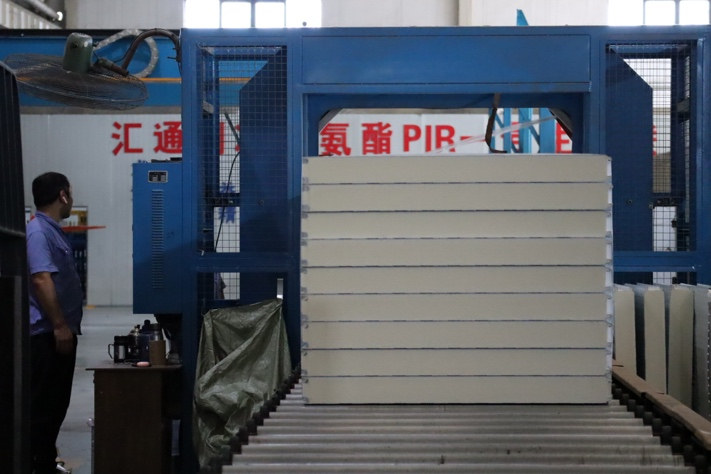
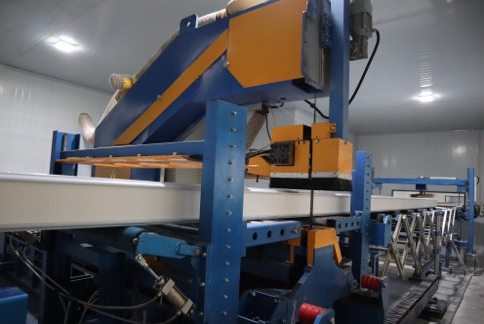
With about 180 workers and 10 QC team, the quality and efficiency are guaranteed of our products. Now, the factory has an existing production site of 60,000 square meters, 4 standardized workshops (expanding up to 8 advanced workshops), high quality and efficient production equipment, as well as advanced production lines and techniques. Our factory mainly produces PIR (Polyisocyanurate) and PU (Polyurethane) sandwich panels, cold storage doors, air coolers, condensers, condensing units, compressor units etc.
Over 28 Years of Engineering Growth and Continuous Technological Evolution.
Our founder started the business from refrigeration equipment marketing and installation.
With our first factory completed in Shaanxi, we produced our first cam-lock sandwich panels.
The second factory in LanZhou completed; our business started to cover the whole north-west market in China.
Followed by larger domestic and international business, the Shaanxi factory relocated to expanded grounds covering 120 acres with 8 advanced workshops.
Integrating advanced technology in the insulation panel industry, we launched our first automatic split-joint production line, beginning a new chapter.
Our second advanced automatic production line went on stream, reaching higher productivity and efficiency with elevated quality standards.
Driven by sustainability goals, we transitioned operations into a fully eco-friendly smart manufacturing facility.
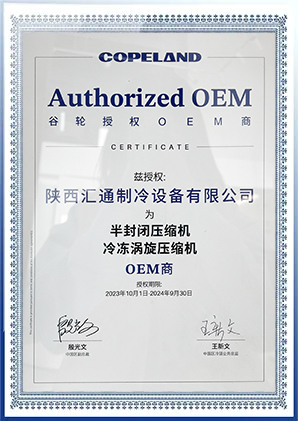
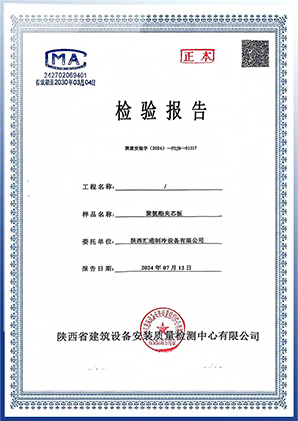
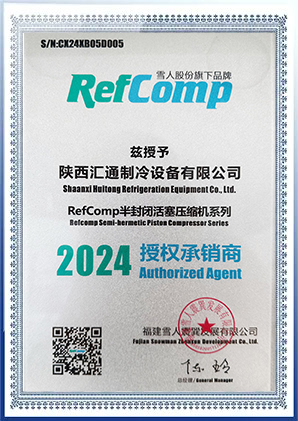
Rigorous International Compliance Confirming Technical Superiority.
Direct Answers from Our Chief Thermal Engineers on Customization, Efficiency, and Logistics.
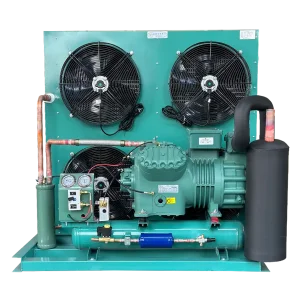
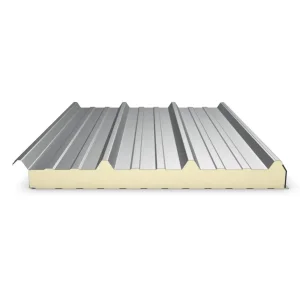
Complete One-Stop Cold Room Infrastructure: Compressors, Evaporators, Doors, and PIR Panels.
 YuanShengHeTong