High-performance condensing units engineered specifically to excel under tropical ambient conditions, high humidity, and intensive thermal loads.
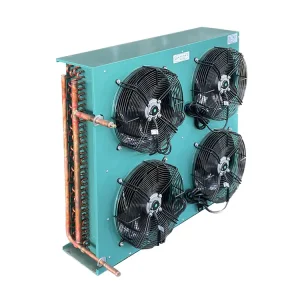
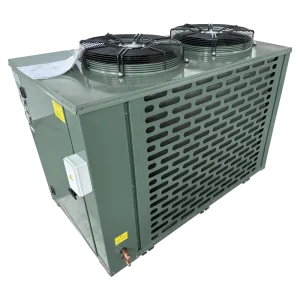
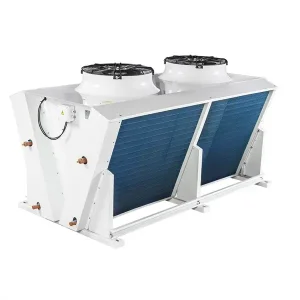
As the recognized commercial capital of Southwestern Uganda, Mbarara serves as the epicenter for agriculture, dairy processing, livestock distribution, and regional trade connecting Uganda with Rwanda, the Democratic Republic of Congo (DRC), and Tanzania. With rapid urban expansion, infrastructure investments in the Mbarara Industrial Park, and the modernization of dairy aggregation facilities along the Biharwe-Ruti corridor, the demand for industrial-grade refrigeration, heavy-duty condensers, and modular cold rooms has reached unprecedented levels.
Operating cold storage infrastructure in Mbarara presents unique thermodynamic challenges. Situated at an elevation of approximately 1,470 meters above sea level with tropical savanna thermal profiles, condensers must withstand elevated ambient operating temperatures, variable humidity cycles, and intense continuous duty cycles without sacrificing Coefficient of Performance (COP) or risking thermal breakdown.
Understanding the physics of refrigerant phase transition under sub-Saharan operational stresses is central to our manufacturing philosophy.
Our FNH, FNV, and FVB condenser series utilize internally rifled high-purity copper tubes. This microgroove design increases internal surface area by up to 35%, breaking fluid boundary layers and accelerating turbulent refrigerant heat exchange. Result: 18% higher heat rejection efficiency compared to conventional smooth-bore copper designs.
In environments subject to atmospheric dust and agro-processing particulate, standard aluminum fins suffer from rapid fouling and oxidation. We offer blue hydrophilic or epoxy-coated aluminum fins that repel moisture buildup, resist airborne chemical attack, and simplify high-pressure coil washing routines.
Equipped with low-noise axial fans engineered with 3D sickle-blade geometry, our condensing units maximize airflow volumetric rates (m³/h) while keeping acoustic emissions minimal. Rated for IP54/IP55 ingress protection to withstand tropical downpours and dust ingress effortlessly.
Bridging advanced manufacturing technology in China with the growing infrastructure requirements of Mbarara and greater East Africa.
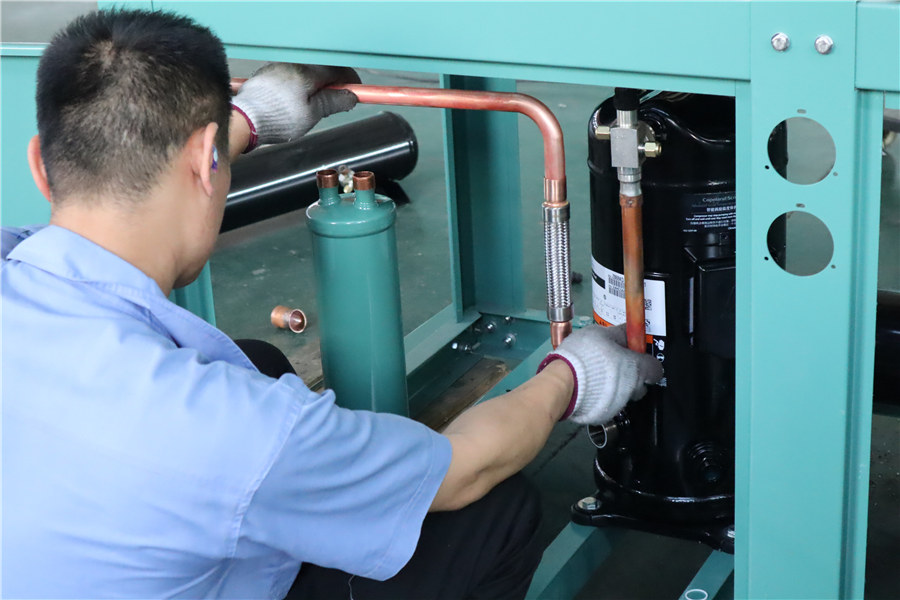
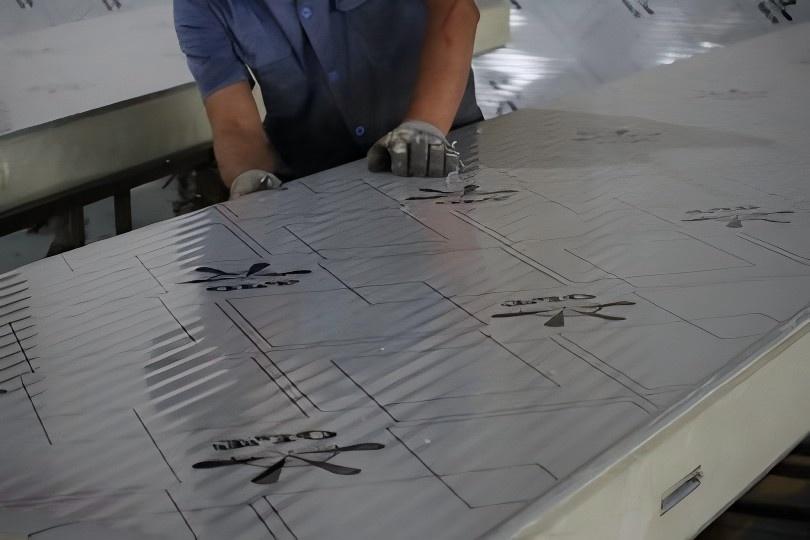
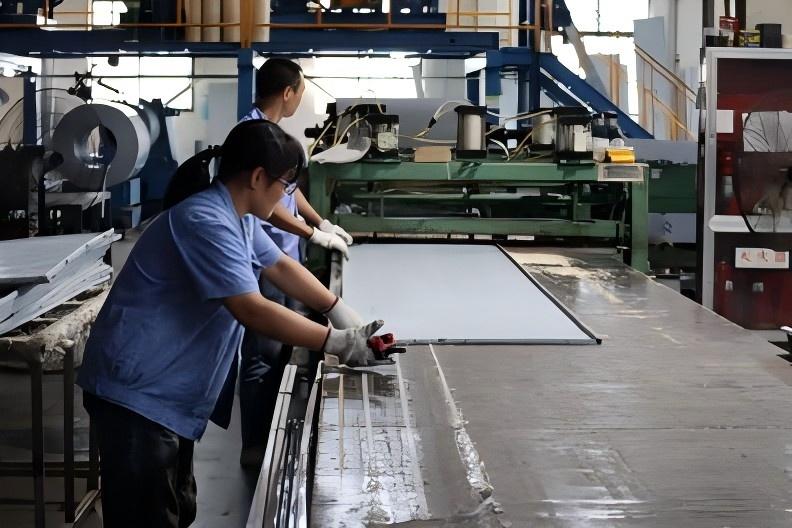
Shaanxi YuanShengHeTong Refrigeration Equipment Co., Ltd. is a premier manufacturing enterprise specializing in continuous insulation panels, automated cold storage doors, air coolers, condensers, and heavy compressor condensing units. Operating across 4 standardized mega-workshops equipped with automated split-joint production lines, our facility seamlessly combines engineering precision with mass production capacity.
For importers, engineering contractors, and plant operators in Mbarara, partnering directly with our factory guarantees full supply chain transparency, zero intermediary markups, standardized ISO/CE manufacturing controls, and short lead times from order placement to containerized shipping via Mombasa or Dar es Salaam ports.
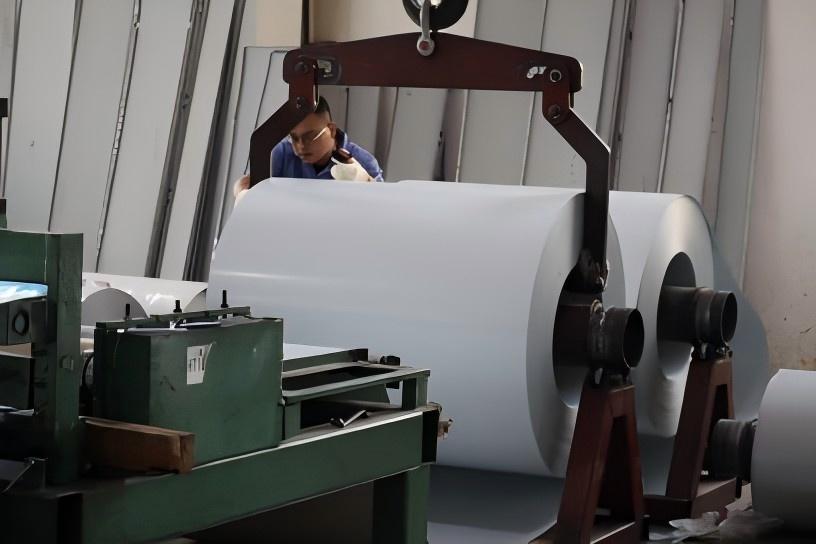
Over nearly three decades of growth, we have evolved from a regional refrigeration installation team into a global exporter of cold storage engineering solutions.
Founder initiates refrigeration equipment marketing, servicing, and local HVAC system installation operations.
First dedicated manufacturing plant completed in Shaanxi, producing precision cam-lock polyurethane sandwich panels.
Second manufacturing complex in LanZhou completed, expanding market dominance across North-West China.
Relocation to 120-acre flagship industrial campus boasting 8 advanced technical workshops to serve global markets.
Commissioning of China's first fully automatic split-joint continuous insulation panel line, elevating precision engineering.
Second continuous automated line comes online, significantly scaling output capacity, dimensional consistency, and density control.
Transition into a zero-emissions eco-friendly modern smart factory, implementing low-GWP refrigerants and energy-efficient heat exchangers for African and global export markets.
From raw milk chilling centers to pharmaceutical storage, our condensers power key economic nodes in Mbarara.
In dairy collection centers along the Mbarara-Masaka highway, fresh raw milk must be rapidly chilled from body temperature (37°C) down to +4°C within two hours to prevent microbial growth. Our high-capacity air-cooled condensing units paired with Copeland or Bitzer compressors deliver the high suction pressures and thermal shock capacity needed for continuous batch chilling.
Modern beef processing operations in Kakoba and surrounding agro-zones rely on deep blast freezing systems (-30°C to -35°C). Utilizing our FNV floor-stand condensers with fluorine defrost evaporators, operators achieve rapid core temperature reduction, locking in product weight, color, and food safety standards for long-distance transport.
As international and regional logistics companies build multi-temperature warehouses in Mbarara, our modular PIR/PU sandwich panels combined with FVB-series V-type air-cooled condensers provide low power-consumption refrigeration infrastructure capable of operating reliably under intermittent grid voltage environments.
Global enterprise buyers and HVAC/R engineering consultants operating in East Africa evaluate condensing units based on long-term total cost of ownership (TCO). Power costs in Uganda represent up to 70% of total lifetime operational expenditures for cold storage facilities. Therefore, selecting high-efficiency heat rejection systems directly impacts bottom-line profitability.
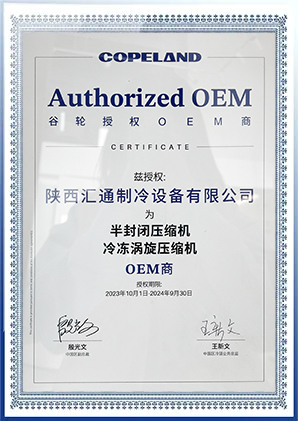
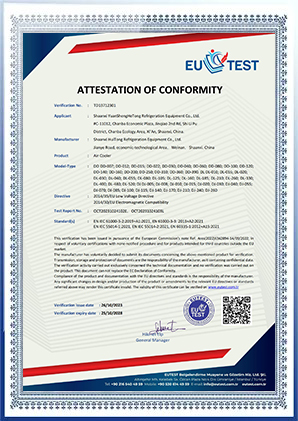
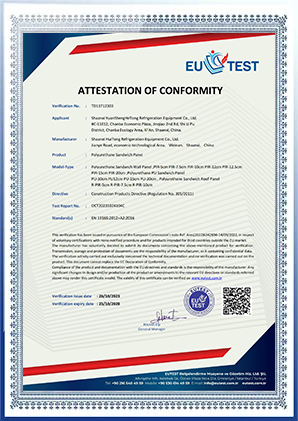
Our quality management system is fully accredited under ISO9001:2015 and CE certification standards, ensuring each unit shipped to Mbarara meets international thermodynamic standards.
Explore our comprehensive lineup of refrigeration hardware designed for exporters, contractors, and industrial buyers across Mbarara and East Africa.
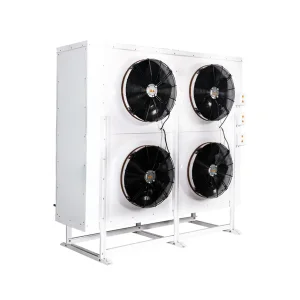
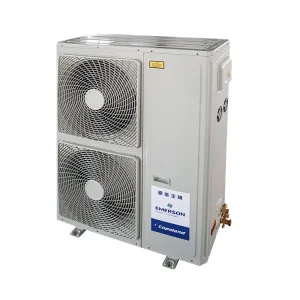
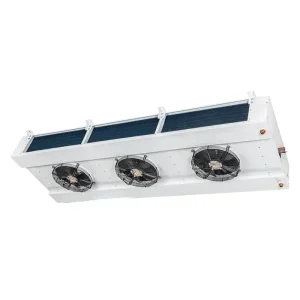
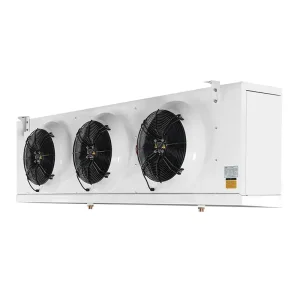
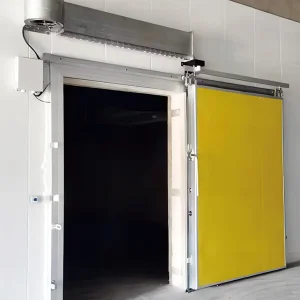
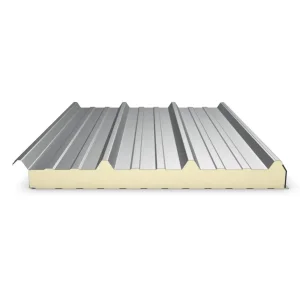
Expert guidance on selecting, sizing, importing, and maintaining industrial condenser systems in Southwestern Uganda.
Consult directly with our senior refrigeration engineers. Whether you need a single OEM condensing unit, a replacement condenser coil, or a complete turnkey cold room system with PIR panels and cold room doors, we deliver direct factory pricing and technical reliability.
Send Inquiry Now YuanShengHeTong